Optimizing Hot Tack Force and Low Seal Initiation Temperature (Low SIT): The Key to Maximizing VFFS/HFFS Automated Packaging Line Productivity
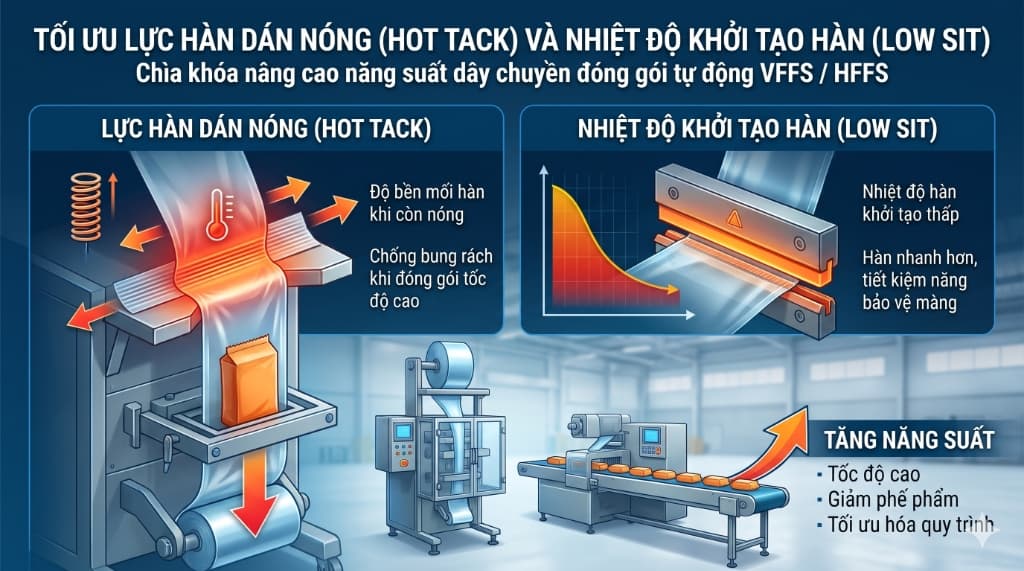
📌 SUMMARY FOR PACKAGING ENGINEERS & LINE MANAGERS: In modern food, FMCG, and agricultural processing plants, the speed of automated Vertical Form-Fill-Seal (VFFS) and Horizontal Form-Fill-Seal (HFFS) packaging lines is often bottlenecked by two heat-sealing parameters: Seal Initiation Temperature (Low SIT) and Hot Tack Strength. This technical analysis explores how NOVAPLEX® 5-layer co-extruded PE film overcomes these constraints to boost line speeds by 15%–25% while ensuring 100% hermetic seal integrity.
1. Speed Bottlenecks on Automated VFFS & HFFS Lines
As FMCG and food manufacturing facilities accelerate automated packaging operations to 80–150 bags per minute, the performance of the inner sealant film becomes the single most critical factor determining Overall Equipment Effectiveness (OEE). When heavy products (e.g., 500g snacks, 1L liquids, or frozen seafood) drop into a bag immediately after the sealing jaws cycle, the bottom seal is still molten. Without sufficient Hot Tack strength (> 4.0 N/15mm), seal failure or micro-leaks immediately occur.
To compensate, machine operators are frequently forced to reduce line speed or excessively raise jaw temperatures. However, excessive heat leads to film shrinkage, cosmetic wrinkling, and severe jaw sticking, driving up scrap rates and causing costly unplanned downtime.
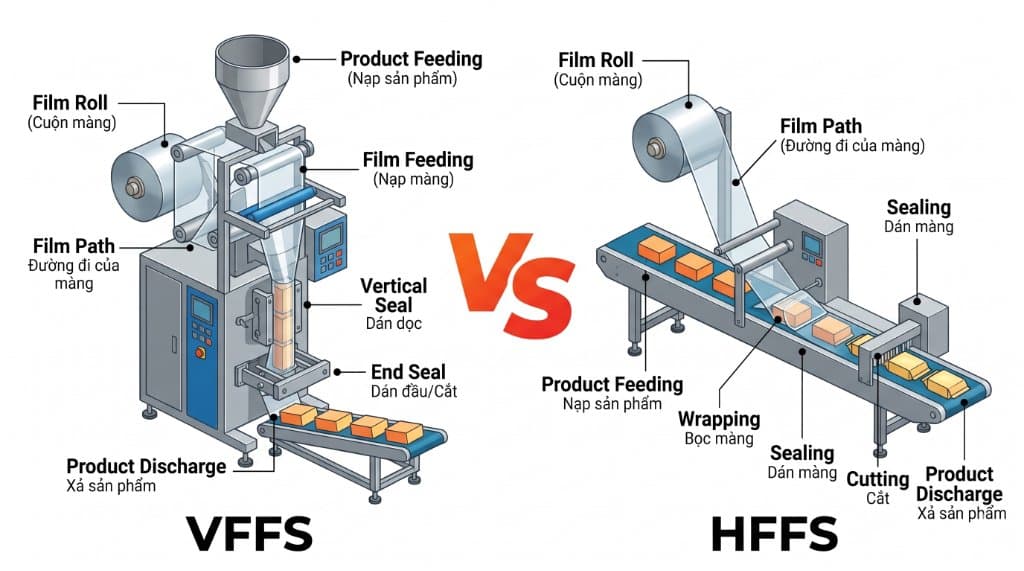
Operational diagram: Vertical Form-Fill-Seal (VFFS) vs. Horizontal Form-Fill-Seal (HFFS) packaging machinery
2. Demystifying Core Heat-Seal Parameters: Low SIT & Hot Tack
Optimizing high-speed cycle times relies on the synergistic control of two physical parameters:
Table 1: Operational Comparison: Standard PE Film vs. Optimized NOVAPLEX® PE Film
| Technical Metric / Performance | Standard PE Film | NOVAPLEX® 5-Layer PE Film | Tangible Factory Benefit |
|---|---|---|---|
| Seal Initiation Temperature (SIT) | 105°C – 115°C | 88°C – 95°C | Saves ~15% heating energy |
| Hot Tack Sealing Force | 1.5 – 2.5 N/15mm | > 4.5 N/15mm | Boosts line speed +15% to +25% |
| Dwell Sealing Time | 0.4s – 0.6s | 0.12s – 0.20s | Significantly shortens cycle time |
3. Engineering Breakthrough of NOVAPLEX® 5-Layer Co-Extrusion
Unlike legacy 3-layer extrusion with restricted polymer stratification, NOVAPLEX® 5-layer blown film utilizes a tailored A/B/C/D/E architecture formulated with specialized virgin polyethylenes: